Guide 14: CNC Threads Explained: Tapped Holes, Thread Milling, and Thread Inserts
This CNC DFM guide compares the three core threading methods—Tapped Holes, Thread Milling, and Thread Inserts—breaking down their costs, advantages, and ideal applications. It provides essential design rules, including optimal thread depth (1.0×–1.5× diameter), hole strategies, and common mistakes to avoid for better manufacturability and lower tooling wear.
Guide 14: CNC Threads Explained: Tapped Holes, Thread Milling, and Thread Inserts
Tapping, Thread Milling & Thread Insert Design | Manufacturing Academy
1. Introduction
Threads are among the most pervasive features in CNC machined parts. Almost every mechanical assembly relies on threaded fasteners to join structural members, secure covers, or align critical sub-assemblies. However, many engineers design threads in CAD without considering the underlying machining mechanics.
Specifying oversized thread depths, unnecessarily long threaded engagement lengths, or non-standard thread profiles can rapidly escalate tooling wear, increase cycle times, elevate scrap rates, and drive up manufacturing costs. Selecting between tapped holes, thread milling, and threaded inserts early in the design stage ensures your components are both cost-effective and structurally dependable.
2. Method 1: Tapped Holes
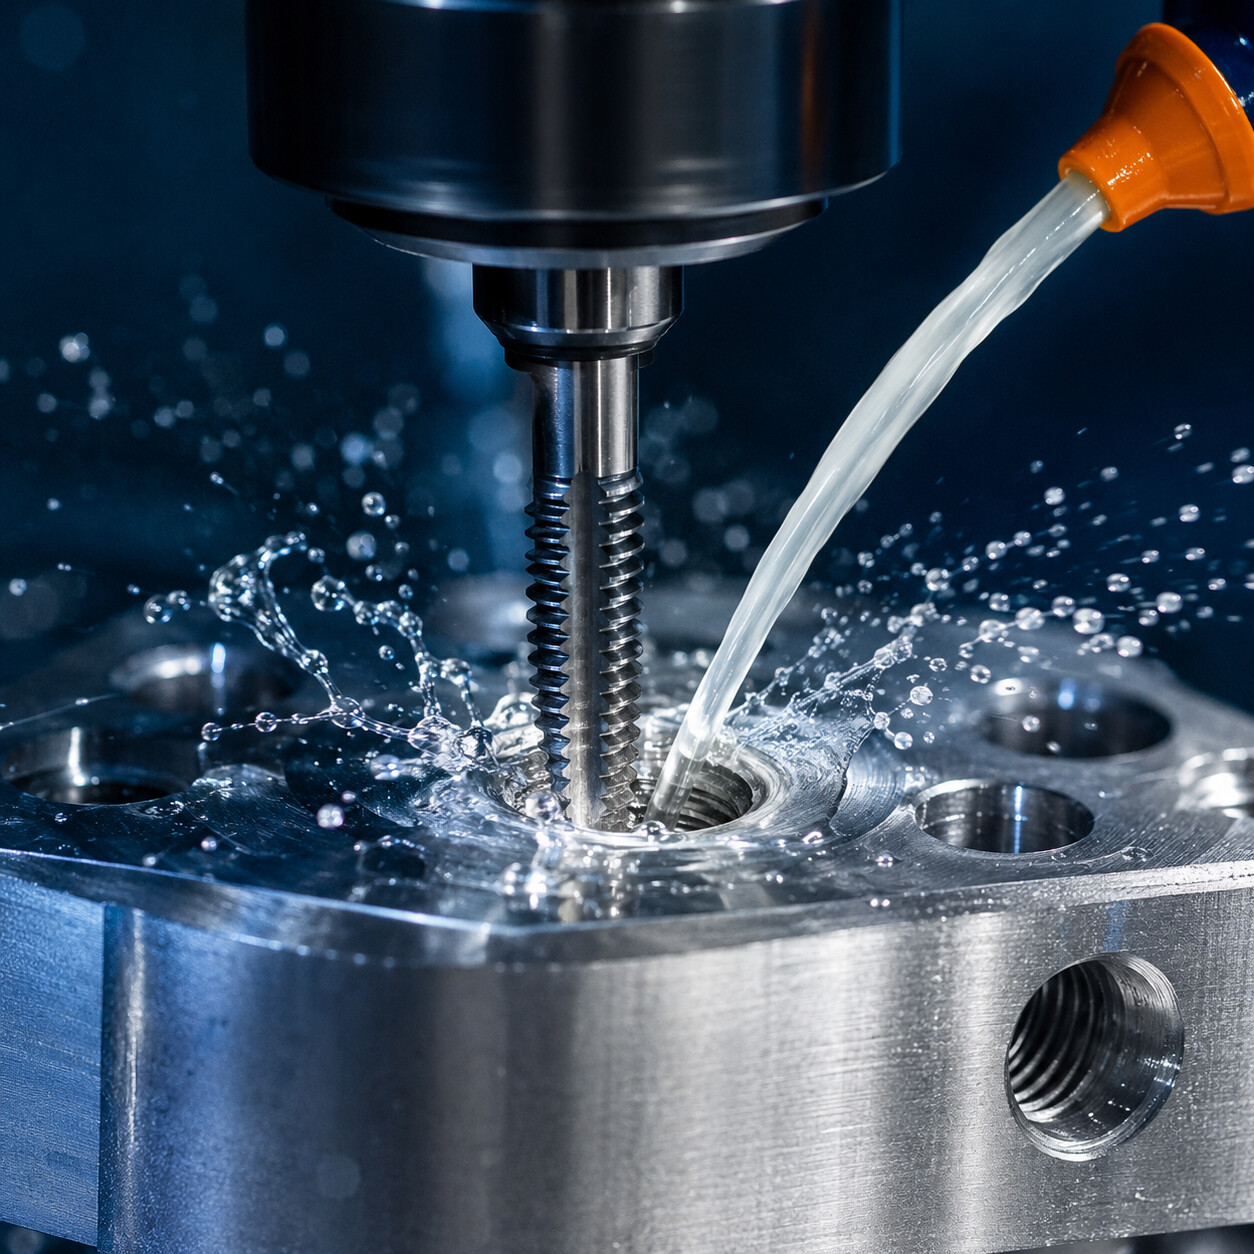
Tapping is the conventional and most widespread method for forming internal threads in CNC machining. After a pilot hole is drilled to the specified tap drill diameter, a cutting or forming tap is driven into the hole to produce the internal thread profile.
Key Advantages:
Rapid Execution: Machining cycle times are extremely short.
Cost-Effective: Minimal tooling investment and standard CAM cycles.
High Repeatability: Ideal for high-volume production runs.
Best Applications:
Aluminum alloys (e.g., 6061-T6, 7075-T6)
Mild steels and stainless steel grades
Standard machine screw sizes (M3 to M12)
General mechanical structural enclosures and plates
3. Method 2: Thread Milling
Thread milling uses a rotating helical cutter on a multi-axis CNC machine to generate internal or external threads via circular interpolation. Unlike tapping, where the tool geometry directly dictates thread pitch and diameter, thread milling offers continuous control over thread dimensions.
Key Advantages:
Dimensional Precision: Allows fine-tuning of thread tolerances and fit classes.
Reduced Tool Breakage Risk: Small chips clear easily; if a mill breaks, it does not lock into the workpiece like a tap.
Multi-Size Versatility: A single thread mill can cut various thread diameters sharing the same pitch.
Blind Hole Safety: Allows full threads closer to the bottom of blind holes without tap chip packing.
Best Applications:
Hardened steels, titanium alloys, and nickel superalloys (Inconel)
Large-diameter threaded features (>M12 / >0.5 inch)
High-value aerospace and medical components where tap breakage causes catastrophic part rejection
4. Method 3: Thread Inserts
When base materials (such as aluminum, magnesium, or engineering plastics) lack the shear strength to endure repeated assembly cycles or extreme clamp loads, post-machining thread inserts are integrated.
Common Thread Insert Types:
Wire Screw Thread Inserts (Helicoil): Diamond-shaped stainless steel wire coils inserted into tapped holes to distribute bolt loads.
Solid Threaded Inserts (Key-Locking / Key-Lok): Heavy-duty solid metal bushings with locking keys for maximum pull-out strength.
Press-Fit & Self-Tapping Inserts: Mechanically anchored inserts installed in ductile metals or rigid polymers.
Heat-Set Inserts: Thermally installed brass inserts for 3D-printed or molded thermoplastics.
5. Process Comparison: Tapping vs. Thread Milling vs. Inserts
Feature Property | Tapped Holes | Thread Milling | Thread Inserts
|
Machining Speed | Very Fast | Moderate to Slow | Requires secondary installation |
Machining Cost | Lowest | Moderate to High | Higher (tooling + hardware + labor) |
Thread Accuracy | Standard (Class 2B / 6H) | High (Class 3B / 4H selectable) | Very High (Stainless insert tolerance) |
Tool Failure Risk | Moderate (tap breakage in tough alloys) | Low (milling cutter clears chips easily) | Low (inserted into standard tapped holes) |
Large Diameters | Requires heavy spindle torque | Excellent & Highly Efficient | Available, but costly in large sizes |
Soft Material Durability | Moderate (susceptible to wear) | Moderate | Superior (prevents thread stripping) |
6. Recommended Thread Depth Rules
A frequent DFM error is specifying excessive thread depth. Engineering tests demonstrate that in metallic materials, 1.0× to 1.5× the screw diameter provides over 90–95% of full tensile fastener strength. Additional depth increases machining risk without structural benefit.
Screw Thread Size | Nominal Diameter | Recommended Thread Depth (1.0x – 1.5x D)
|
M4 | 4 mm | 4 mm – 6 mm |
M5 | 5 mm | 5 mm – 8 mm |
M6 | 6 mm | 6 mm – 9 mm |
M8 | 8 mm | 8 mm – 12 mm |
M10 | 10 mm | 10 mm – 15 mm |
7. Blind Holes vs. Through Holes
Whenever practical, design through-holes for threaded features. Through-holes facilitate chip evacuation, allow chips to exit cleanly, reduce tap wear, and lower unit cost.
When blind holes are necessary, ensure adequate drill point clearance below the effective thread length (typically 0.5× diameter extra depth) to accommodate tap lead chamfers and chip packing.
8. Standard Thread Profiles
Always specify standardized thread profiles across your designs:
ISO Metric (e.g., M6x1.0, M8x1.25)
Unified National Coarse/Fine (UNC/UNF)
Avoid custom pitch profiles or non-standard thread forms unless strictly required for proprietary sealing mechanisms.
9. Recommended Design Practices (DFM Checklist)
✔ Use Tapped Holes for standard production in aluminum, steel, and general assemblies.
✔ Use Thread Milling for large-diameter holes, titanium, or high-value aerospace parts.
✔ Use Thread Inserts in soft alloys subjected to frequent disassembly cycles.
✔ Limit Thread Depth to 1.0×–1.5× fastener diameter.
✔ Include Lead-In Chamfers: Specify a 90° chamfer at every hole mouth to guide taps and prevent thread burrs.
✔ Favor Through-Holes: Design through-holes over blind holes wherever physical geometry permits.
10. Common Thread Design Mistakes
Excessive Thread Depth: Designing 3x–4x diameter thread depth increases tap wear and tool breakage risks.
Micro Threads (< M3): Sub-M3 threads require fragile tooling and dedicated micro-tapping operations.
Missing Hole Entrance Chamfers: Leads to burr formation, difficult screw starting, and potential cross-threading.
Unnecessarily Tight Thread Tolerances: Specifying Class 3B tolerances when Class 2B is sufficient increases inspection and machining costs.
11. Conclusion
Optimizing thread design is one of the easiest ways to improve CNC manufacturability and prevent unexpected tooling expenses. By matching the right threading method to your material, controlling thread depth, and adhering to standardized threads, you guarantee durable assemblies at optimal unit costs.
Need Help Designing Threaded Features?
Our engineering team evaluates threaded holes, fastener selection, and machining strategies during every DFM review. We help optimize your designs for manufacturability, thread engagement, and long-term joint reliability.
Upload your CAD models today for professional DFM feedback and a fast CNC quote.