Guide 16: CNC Datum Selection: How Proper Reference Surfaces Improve Accuracy
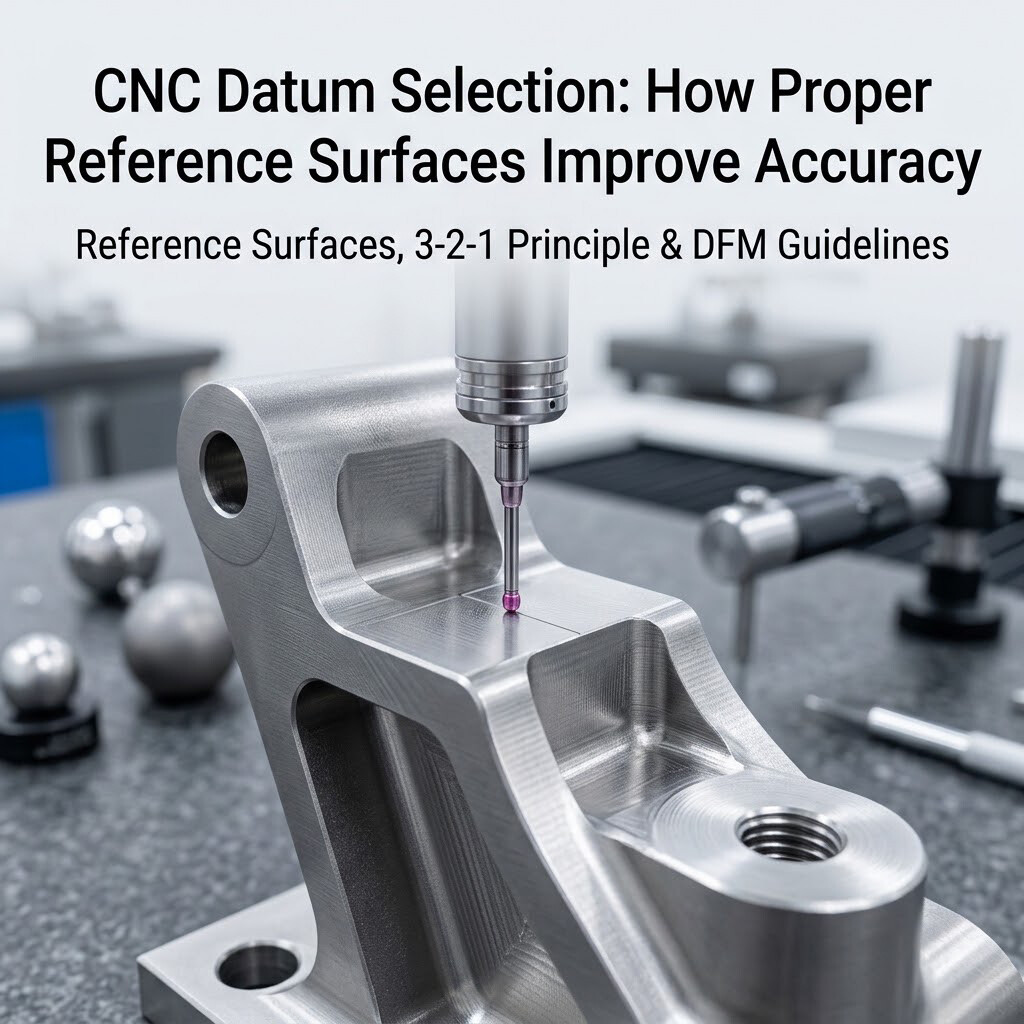
This guide covers CNC datum selection, the 3-2-1 locating principle, and DFM best practices to eliminate tolerance stack-up and enhance machining accuracy.
Guide 16: CNC Datum Selection: How Proper Reference Surfaces Improve Accuracy and Reduce Manufacturing Errors
Reference Surfaces, 3-2-1 Principle & DFM Guidelines | Manufacturing Academy
1. Introduction
Even the most advanced multi-axis CNC machining center cannot produce accurate parts without a logically defined reference system. Every dimension on an engineering drawing originates from a reference feature. Every CNC cutting operation requires a zero coordinate (work coordinate system / WCS). Every CMM inspection routine measures features relative to defined reference surfaces.
That reference system is established by datums. Flawed datum selection introduces tolerance stack-up, mandates extra machine setups, complicates quality inspection, and causes part rejections. Selecting the right datums during early CAD design ensures components are straightforward to machine, inspect, and assemble reliably.
2. What Is a Datum?
In GD&T (Geometric Dimensioning and Tolerancing) and mechanical engineering, a datum is a theoretically exact point, line, axis, or plane from which the location and geometric characteristics of part features are established.
In practical CNC manufacturing, theoretical datums are represented by physical part surfaces (known as datum features). These physical reference surfaces contact fixture locators, vise jaws, or inspection tables during:
Raw Material Setup & Workholding (Fixturing)
CNC Machining & Work Coordinate System (WCS) Alignment
Quality Inspection & CMM (Coordinate Measuring Machine) Measurement
Final Product Assembly
3. Why Datum Selection Is Critical
Proper datum selection guarantees that:
Critical Dimensions Remain Consistent: Tight-tolerance features maintain precise spatial alignment.
Setups Are Repeatable: Variations between different machining setups or operators are minimized.
Inspection Mirrors Design Intent: Quality control verifies dimensions against functional assembly interfaces.
Manufacturing Costs Drop: Fixture design is simplified, setup times decrease, and scrap rates fall.
4. The 3-2-1 Locating Principle
To fully constrain a solid body in 3D space, all six degrees of freedom (3 translational axes + 3 rotational axes) must be eliminated. Precision CNC fixturing relies on the 3-2-1 Locating Principle:
Primary Datum (Plane A): Constrained by 3 contact points. Establishes the main orientation plane and eliminates 3 degrees of freedom (1 translation, 2 rotations).
Secondary Datum (Plane B): Constrained by 2 contact points. Perpendicular to Plane A; eliminates 2 degrees of freedom (1 translation, 1 rotation).
Tertiary Datum (Plane C): Constrained by 1 contact point. Perpendicular to both A and B; eliminates the final degree of freedom (1 translation).
5. Selecting Primary, Secondary, and Tertiary Datums
Datum Role | Contact Points | Ideal Surface Characteristics | Typical Examples
|
Primary Datum (A) | 3 Points | Largest flat surface, highly rigid, functionally critical | Base plate face, mounting flange, housing deck |
Secondary Datum (B) | 2 Points | Long side face or precision bore, perpendicular to Primary | Long side edge, precision dowel hole axis |
Tertiary Datum (C) | 1 Point | Short side face or end edge, perpendicular to Primary & Secondary | Short end face, secondary locating pin center |
6. Functional Datums vs. Manufacturing Datums
Engineers must distinguish between two key reference concepts:
Functional Datums: Features that define how the part locates, mates, and functions inside the final assembled product (e.g., bearing seats, precision pilot bosses, bolt circle centers).
Manufacturing Datums: Features selected specifically to simplify clamping, probing, and indexing during CNC machining operations.
DFM Gold Rule: Whenever possible, align manufacturing datums directly with functional datums. This eliminates transfer errors caused by switching references between machining setups and final inspection.
7. Avoiding Chained Dimensions & Tolerance Stack-Up
A frequent drafting error is chained dimensioning (dimensioning Feature B from Feature A, then Feature C from Feature B). In chained dimensioning, manufacturing tolerances accumulate cumulatively across features, leading to out-of-spec parts.
Baseline / Datum Dimensioning: Always reference critical features directly back to a common datum. This ensures individual feature tolerances remain independent, preventing tolerance stack-up.
8. Designing Datum-Friendly Geometry
Good datum surfaces should exhibit these characteristics:
Flat and Rigid: Large, flat surfaces resist clamping deflection.
Accessible: Easily reached by fixture clamps, edge finders, and CMM touch probes.
Machined Early: Machine primary datum surfaces in the first setup (OP10) so subsequent operations reference precision surfaces.
Avoid using as datums: Small fillet radii, raw cast textures, draft-angled surfaces, thin un-supported walls, or cosmetic exterior panels.
9. Datum Strategy in Multi-Setup Machining
Complex parts often require multiple operations (e.g., OP10, OP20, OP30). Changing datum reference schemes between setups introduces cumulative positioning errors. Maintaining a consistent primary datum system across all setups ensures high accuracy and simplifies CAM programming.
10. Common Datum Selection Mistakes
Referencing Flexible / Thin-Walled Surfaces: Clamping onto compliant walls causes elastic deflection; once unclamped, the surface spring-backs out of tolerance.
Selecting Unmachined / Raw Surfaces: Using unmachined stock edges as references for tight-tolerance secondary features introduces stock thickness variations.
Multiple Independent Reference Systems: Creating conflicting datum schemes on a single drawing causes confusion between machinists and quality inspectors.
Ignoring Assembly Interfaces: Selecting datums that do not correspond to how the part mates in assembly leads to alignment issues during build up.
11. Recommended Design Practices (DFM Checklist)
✔ Select Large, Rigid Surfaces as primary datums to ensure stable fixturing.
✔ Align Manufacturing & Functional Datums: Use functional mounting faces as your CNC machining zero references.
✔ Use Baseline Dimensioning: Dimension critical features directly from primary datums to avoid tolerance accumulation.
✔ Machine Primary Reference Planes First (OP10): Establish clean, flat reference surfaces before cutting tight features.
✔ Maintain Scheme Consistency: Keep datum references uniform across drawing views and setup operations.
12. Conclusion
Datum selection is the foundation of precision CNC manufacturing and quality control. By establishing clear, accessible, and functional reference surfaces early in CAD design, engineers minimize tolerance stack-up, reduce setup times, simplify CMM inspection, and ensure parts assemble perfectly every time.
Need Help Optimizing Your Part for Manufacturing?
Our engineering team evaluates datum strategies, GD&T schemes, tolerance stack-ups, and fixturing requirements during every DFM review. We help ensure your parts are easy to machine, straightforward to inspect, and ready for reliable production.
Upload your CAD files today to receive expert DFM feedback along with your CNC quotation.