Guide 01: Why Is My CNC Quote So Expensive?
High CNC machining quotes are typically driven by design complexity, material choice, and setup time—not just supplier margins. This guide breaks down the core factors affecting your pricing and offers practical engineering tweaks to eliminate unnecessary manufacturing costs.
Guide 01: Why Is My CNC Quote So Expensive?
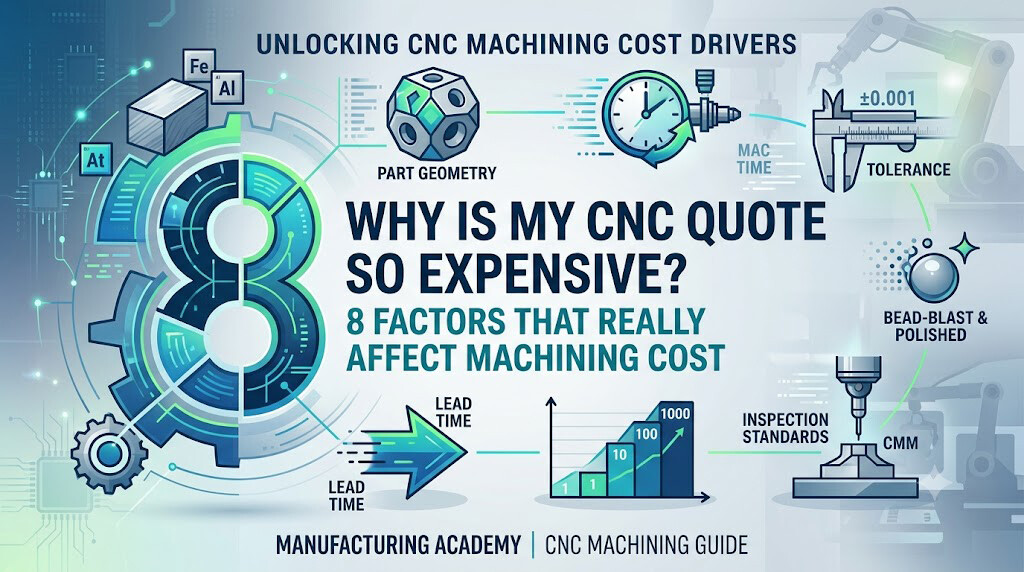
8 Factors That Really Affect Machining Cost | Manufacturing Academy
CNC quote variations usually stem from engineering factors rather than profit margins. Understanding these key drivers helps optimize designs, compare suppliers, and eliminate unnecessary manufacturing expenses.
1. Material Selection & Machinability
Material dictates allowable cutting speeds (SFM), tool wear rates, coolant usage, and cycle time. Harder materials increase tool wear and require slower feeds/speeds, directly extending production time.
Material | Machinability | Relative Cost | Primary Cost Drivers |
Aluminum 6061 | Excellent (100%) | Low | Fast cutting speeds, minimal tool wear, abundant raw stock. |
Brass (C360) | Excellent (100%+) | Low – Medium | High cutting speeds; higher raw material cost per kg than aluminum. |
Mild Steel (1018/A36) | Good (60–70%) | Medium | Moderate speeds; low raw stock cost, higher cycle time than aluminum. |
Stainless Steel 304 | Fair (45–50%) | High | Work-hardening behavior, slower feeds, frequent tool insert changes. |
Titanium (Ti-6Al-4V) | Poor (20–30%) | Very High | High heat generation, specialized tooling required, costly raw material. |
💡 Cost Tip: Switching from Stainless Steel 304 to Aluminum 6061/7075 cuts raw material and cycle costs by up to 50–70% when operating conditions allow.
2. Part Complexity & Geometry
Complex geometries require sophisticated toolpaths, multiple setups, specialized workholding, and frequent tool changes.
· Deep Cavities & Pockets: Require long end mills prone to deflection/vibration, forcing slower cuts.
· Thin Walls (< 1.5 mm): Flex during machining; require light multi-pass cuts to avoid distortion.
· Sharp Internal Corners: End mills are round; sharp vertical corners require micro-tools or EDM.
· Multi-Axis Organic Surfaces: Contoured surfaces require 4/5-axis CNCs and fine finishing toolpaths.
· Undercuts: Demand custom cutters (lollipop, T-slot) or specialized indexing setups.
3. Machining Cycle Time
Machine hourly rates account for capital depreciation, power, overhead, and skilled labor. Primary drivers include:
1. Material Removal Rate (MRR): Volume of stock material milled away.
2. Feeds & Speeds: Dictated by material hardness and tool geometry.
3. Feature Density: Total count of holes, threads, pockets, and chamfers.
4. Toolpath Optimization: CAM software limits based on geometric complexity.
4. Tolerance Requirements
Over-specifying tight tolerances is a primary cause of inflated quotes. Restrict tight tolerances strictly to critical functional features.
Tolerance Class | Typical Value | Machining & QC Impact | Cost Multiplier |
Standard Commercial | ±0.10 mm (±0.004″) | Standard tooling, high-speed cutting, routine caliper check. | 1.0x (Baseline) |
Fine Tolerance | ±0.05 mm (±0.002″) | Finishing passes, thermal control, gauge block inspection. | 1.3x – 1.5x |
Precision / High Tight | ±0.01 mm (±0.0004″) | Grinding/boring, temperature-controlled room, CMM verification. | 2.0x – 3.0x+ |
📐 Design Recommendation: Only specify tight tolerances (±0.01 mm) on critical functional features (bearing seats, locating pins). Leave other dimensions to standard block tolerances (±0.10 mm).
5. Surface Finish & Secondary Post-Processing
Every post-processing step introduces additional handling, chemical fees, logistics, and QA steps.
· As-Machined (Ra 3.2 µm): Standard machine output; lowest cost option.
· Bead Blasting (Ra 1.6 µm): Uniform satin-matte texture; removes mild tool marks.
· Anodizing (Type II/III): Electrochemical coating for corrosion resistance, insulation, and color (Aluminum).
· Powder Coating / Painting: Thick protective layer for heavy wear; requires tolerance masking.
· Electropolishing & Passivation: Removes free iron from stainless steel for maximum corrosion resistance.
· Polishing / Mirror Finish: Labor-intensive manual or mechanical buffing for optics/aesthetics.
6. Order Quantity & Batch Economies of Scale
Fixed Non-Recurring Engineering (NRE) costs (CAM programming, machine setup, fixturing, FAI) are amortized over total order volume.
Order Batch Size | Setup / NRE Cost Share | Unit Machining Cost | Relative Unit Price |
1 Unit (Prototype) | 100% of setup cost | Standard rate | Highest (100%) |
10 Units (Small Batch) | 10% per unit | Slight efficiency gains | Moderate (~40% off) |
100 Units (Medium Run) | 1% per unit | Optimized toolpaths & fixtures | Significant (~70% off) |
1,000+ Units (Production) | Negligible per unit | Dedicated automation fixtures | Lowest (~80–85% off) |
7. Inspection & Quality Assurance Standards
· Standard Quality Control: Hand tools (calipers, micrometers, thread gauges) & visual check included.
· Advanced Precision Inspection: CMM touch-probe scanning, dimensional reports, MTRs, and FAI (AS9102) docs (adds 15–30% to total cost for aerospace/medical parts).
8. Lead Time & Delivery Urgency
Expedited orders disrupt schedules, require overtime, and incur premium shipping fees. Standard lead times enable optimized machine scheduling and batching.
Actionable DFM Strategies to Reduce CNC Costs
Implementing key Design for Manufacturability (DFM) rules during initial design yields substantial savings without compromising mechanical performance:
Design Parameter | High-Cost Design Choice | Cost-Effective Alternative (DFM) |
Material Selection | Hard-to-machine alloys (Titanium, Inconel) | Standard grades (Aluminum 6061-T6, Mild Steel 1018) |
Internal Corners | Sharp 90° internal vertical corners | Add floor-to-wall radii (radius ≥ 1/3 pocket depth) |
Pocket Depth | Deep pockets (> 4x tool diameter) | Limit cavity depth to ≤ 3x–4x end mill diameter |
Tolerances | Blanket tight tolerances (±0.01 mm everywhere) | Tight tolerances only on mating surfaces; standard ±0.10 mm elsewhere |
Wall Thickness | Ultra-thin walls (< 0.8 mm) | Maintain minimum wall thickness ≥ 1.5 mm for metals |
Setups | Features on 5–6 faces requiring multi-setups | Align features on 1–2 primary directions to minimize repositioning |
Why Supplier Quotations Vary
Quotations differ based on shop capabilities (5-axis vs 3-axis), CAM expertise, raw material purchasing power, current shop capacity/backlog, and QA infrastructure (ISO/AS9102). A lower quote isn't always best if it risks delivery delays or out-of-spec parts.
Conclusion & Key Takeaways
· Material & Machine Time: Dominant cost drivers in CNC production.
· Geometry Simplification: Eliminate deep pockets and sharp internal corners to cut tool/programming costs.
· Targeted Precision: Apply tight tolerances only where functionally necessary.
· Batch Aggregation: Amortize NRE/setup costs over higher volume runs.
· Early DFM: Optimizing CAD prior to quoting yields maximum long-term ROI.
Next Guide in Series: Guide 02 — CNC Machining Tolerances Explained: How Precise Does Your Part Really Need to Be?